UV printing smart home device housings / BUYER GUIDE
UV Printing for Smart Home Device Housings: From Artwork Brief to Batch Control
A practical B2B guide to UV printing smart home device housings: sample inputs, factory testing, artwork control, inspection and export preparation for flat plastic products.
Introduction
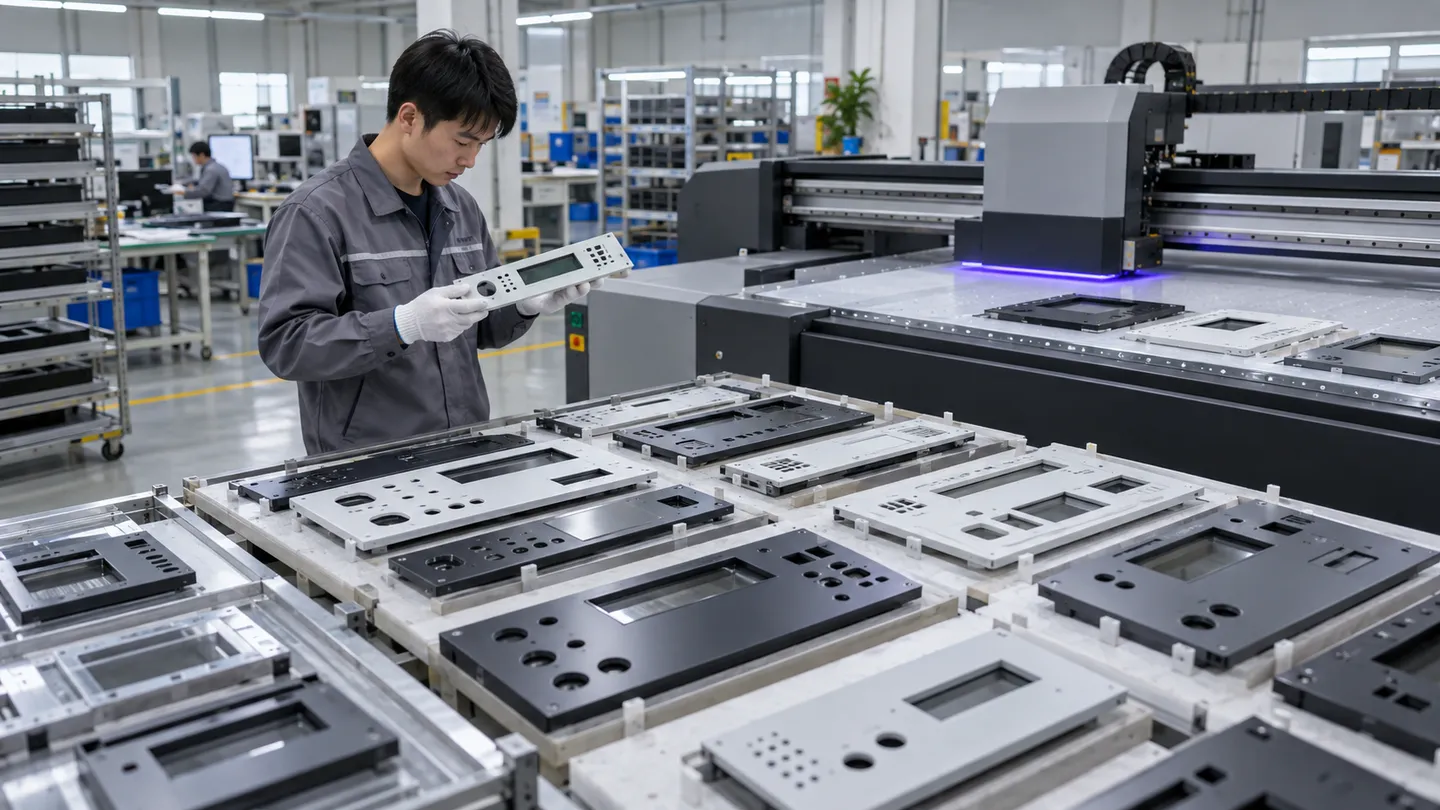
UV printing smart home device housings should be qualified on the real production component, rather than from a material label, a digital rendering or a generic coupon. For flat smart-home device housings, hub covers and wall-mounted accessory panels, PaintNex begins with the final blank, a marked printable zone, the released artwork, handling expectations and the buyer's written acceptance criteria. This guide explains how a procurement team can convert those inputs into a defensible sample and an inspectable batch plan.
Direct answer for buyers
The practical question is whether brand graphics, indicator zones, multilingual variants and retail-ready pack-out can be assessed on the actual component before production. A dependable answer comes from a product-specific trial: use the intended blank, its final surface, the correct artwork revision, a repeatable orientation and the agreed handling or packing conditions. It does not come from a blanket statement that one material name is always compatible.
Why the actual moulded part matters
Plastic parts do not behave as rigid metal coupons. Dimensions, form and local position can move with resin behaviour, shrinkage, tooling, cooling and geometry. ISO 20457:2026 describes a plastics-specific approach to moulded-part tolerances and acceptance conditions. For decoration, this means the fixture and artwork safe area should follow the production part, not an assumed nominal outline.
Inputs to send before feasibility review
| Buyer input | Why it changes the review | Factory output |
|---|---|---|
| Production-equivalent blank | Reveals the true surface, texture and local geometry | Usable print area and fixture reference |
| Released artwork | Controls language, colours, white layers and clear zones | Revision-controlled proof and layer plan |
| Assembly and handling brief | Identifies openings, contact areas and exclusions | Sample test and inspection points |
| Quantity and delivery plan | Shapes tooling, in-process checks and packing | Practical batch and shipment plan |
Material, finish and graphic questions
The resin family is only the first line of the specification. Pigment, mould texture, coatings, films, recycled content, processing history and even a moulder change can alter the visible result. Mark cut-outs, clips, windows, raised features, contact areas and cosmetic zones on the drawing. Ask the factory to confirm what remains printable, what needs an artwork keep-out, and what must be reviewed after assembly.
Define the viewing condition
Colour and finish should be judged against a retained approved part under an agreed viewing condition. This can include neutral lighting, a defined viewing distance and the intended front face. Gloss is not the whole visual story: ASTM D523 addresses specular gloss measurement, while texture and reflection haze can still influence the apparent result. Do not assign an unverified numeric tolerance to a component before the responsible quality parties agree how it will be measured.
Keep compliance content with its owner
If the artwork contains regulatory, service, warning, ESD or localized information, the buyer should supply the approved content and name the accountable product owner. A print factory can control the supplied graphic's position and appearance; it should not infer the legal or technical meaning of an icon. For ESD-sensitive equipment, the ESD Association's ANSI/ESD S8.1 overview distinguishes symbols with different meanings.
Factory testing and sample approval
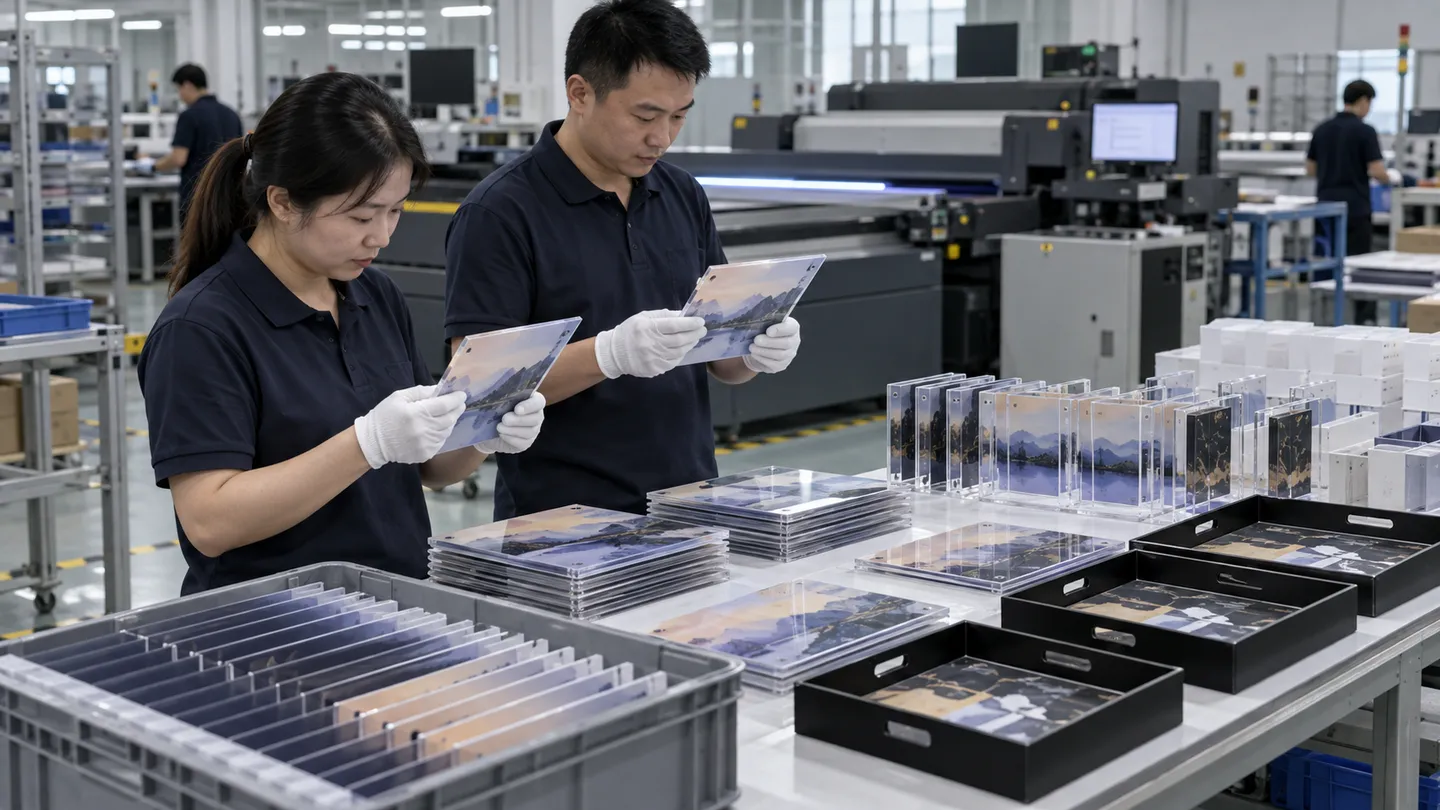
Factory testing should reproduce the variables that matter: the intended blank, final finish, printable orientation, artwork revision, fixture location, white or varnish layers where required, and representative handling. Review placement, edge quality, visible finish, clear zones and packing contact on the physical part. Retain the accepted first-off with a short record of the part version, artwork revision and orientation.
When an adhesion comparison is relevant, agree the exact substrate, surface condition, sample preparation, tape, method and pass/fail rule before testing. ASTM D3359 notes that substrate and surface preparation materially affect coating adhesion, and it identifies limitations of tape methods. Treat the result as a controlled comparison for the specified system, not a universal service-life claim.
Product-specific decisions before artwork release
Separate functional and cosmetic zones
Start by mapping the front face into zones. A cosmetic zone is where a buyer expects a controlled appearance; a functional zone may include a window, sensor, touch area, connector, fastener, latch, light path or assembly datum. The two can overlap visually, so the drawing should make the decision explicit. A printed graphic must never be used as a substitute for an engineering clearance or product-function review.
For flat smart-home device housings, hub covers and wall-mounted accessory panels, the most useful artwork file is accompanied by a simple placement drawing. It identifies the printable zone, a conservative safe area, the part orientation, exclusions and any reference edges used for inspection. That information lets the factory build the fixture and lets an overseas buyer assess the first-off from the same evidence.
Make colour approval traceable
Colour requests are often expressed as a brand reference, a screen image or an informal comment. None of these is enough by itself for batch control. If a specific reference is important, provide the source file, intended substrate, white-base expectation and viewing condition. Keep a signed or otherwise recorded visual approval on the actual component rather than trying to reconstruct it from an email screenshot.
The same discipline applies to matte, gloss, texture and opacity. One component may make a colour look different from another, even where the artwork data is identical. The buyer should decide whether the priority is a visual match, a graphic hierarchy or an agreed production range, then state that priority before the first sample is reviewed.
Plan for change control early
A tool revision, resin supplier change, coating update, changed moulder, different artwork language or altered packaging can all invalidate assumptions in a prior approval. Change control does not have to be bureaucratic: identify the changes that touch the printable face or handling path, compare a new first-off with the retained reference and record the disposition before bulk production resumes.
This is especially important when the buyer expects a family of parts to share one visual identity. Similar housings can have different local geometry, window positions and textures. Approving one size or colour does not automatically approve every member of the family. A short matrix of part number, artwork, finish and approval status is more reliable than a verbal "same as before" instruction.
Inspection language that production teams can use
An inspection standard should be concise enough to use at the line. State the reference sample, the visible face, the artwork revision, permitted and prohibited areas, viewing condition, key placement dimensions if applicable, and the packing configuration. Avoid broad descriptions such as "premium" or "perfect"; they cannot be inspected consistently by two different teams.
Where buyer and supplier use sampling, agree the sample quantity, defect categories and disposition before inspection. The objective is not to create a universal quality claim; it is to make the current order inspectable. A shipment inspection should preserve the same reference that was used in factory testing, so a discrepancy can be discussed against a shared physical and documentary record.
What a useful shipment record contains
A practical record can include photos of the approved first-off and representative batch, part and artwork revision, inspection date, observed result, packing photos and any deviation disposition. It should not replace the buyer's own regulatory, engineering or safety obligations. It gives the purchasing team a clear trail for the decoration work that was actually reviewed.
For direct-to-object decoration, document the product application as well as the print. A faceplate may look acceptable on its own but be obscured after assembly; a presentation tray may look correct until stacked; a control overlay may need a clear window that is invisible in an isolated artwork proof. Ask to see the finished component in its intended context before final release when that context affects acceptance.
How procurement should hand off the project
The purchasing brief should give technical and commercial teams the same starting point. Include part number and revision, material and surface declaration if available, artwork revision, finish intent, quantity, destination, requested date, inspection owner and packing expectation. Where the buyer has a drawing, show which features are cosmetic reference edges and which are functional exclusions. This avoids asking a factory to make assumptions that cannot later be traced to a customer requirement.
Installation preparation also matters when the decorated part will move into a larger assembly. Tell the factory whether the component is supplied loose, assembled, protected by film, or handled with a particular fixture after printing. A print process may be technically feasible on the flat face but unsuitable at a given point in the assembly sequence. Reviewing the hand-off between printing, assembly and packing is cheaper than resolving a cosmetic issue after an order has been completed.
Use the sample to answer specific questions
Write down what the sample is meant to prove. Examples include graphic placement relative to a window, readability of a supplied code at the intended viewing distance, visibility of a white layer on the chosen substrate, compatibility with a nominated cleaning step, or whether packing dividers contact the printed face. A sample cannot prove every imaginable service condition, especially if that condition was not part of the brief. It can provide a clear decision for the agreed product, artwork and handling plan.
If a sample exposes a concern, record whether the next action is an artwork change, a fixture change, a blank-part change, a revised packing method or an additional test agreed by the responsible parties. That keeps the corrective action connected to its cause. It also stops a visual issue from being incorrectly described as a generic printer or ink failure when the issue may be local geometry, an unapproved coating or a contact point outside the original print-safe area.
A practical buyer checklist before purchase order release
- Confirm the component version and quantity match the approved sample request.
- Release the exact artwork file, language variant and source of all required icons or information.
- Mark printable areas, clear zones, contact surfaces and functional exclusions.
- Agree the first-off reference, visible inspection condition and any specifically requested comparison test.
- Confirm fixture orientation, in-process check points, packing protection and shipment-inspection timing.
- Establish how revisions and deviations will be communicated before an order moves to batch production.
This checklist does not transfer product design, legal, regulatory or end-use responsibility to the decoration supplier. It gives procurement a more complete record of the information that a factory needs to execute the requested visual work. The more faithfully the approval part matches the shipped part, the more useful the retained sample becomes when the batch is reviewed.
Mid-article CTA: Request a Product Review
Send PaintNex the physical blank or an approved drawing, the resin and finished-surface information, marked print area, released artwork, quantity, expected handling and packing requirements. We can prepare a product-specific sampling, fixture and inspection brief. Start with our UV-printable materials buyer guide and artwork and fixtures guide if the project inputs are still being assembled.
From approved sample to repeatable batch
1. Freeze the part and artwork version
Record the component revision, surface finish, artwork file and print orientation. When any one changes, compare the new condition with the retained approved first-off before relying on a previous approval.
2. Validate the fixture on representative blanks
Check more than one blank in the intended fixture. A part can sit differently because of local form, gates, tooling variation or assembly features. A fixture supports repeatable placement; it does not erase the need to identify variation that affects the cosmetic zone.
3. Inspect where the buyer will look
Agree the visible face, inspection lighting, viewing distance and defects that matter. Inspect representative pieces for artwork version, position, edge quality, colour appearance, unwanted marks and excluded functional zones. Use a documented quality-control checklist, not a last-minute visual impression.
4. Include pack-out in shipment inspection
The decorated face can be acceptable at the press and still be damaged by stacking, dividers, bags or carton movement. During shipment inspection, review product protection, carton arrangement and representative finished pieces together. Our export packing guide explains the questions worth closing before release.
Common procurement mistakes
| Shortcut | Why it causes risk | Better control |
|---|---|---|
| Approving a coupon only | It hides real geometry and surface variation | Approve the production-equivalent component |
| Sending artwork without keep-outs | It can place graphics over windows or contact zones | Mark printable and excluded regions |
| Treating a material name as a pass result | Coatings and moulding conditions vary | Test the exact part version |
| Inspecting only before packing | Contact damage can occur after decoration | Run a packing trial and shipment inspection |
FAQ
Can this type of part be approved from a rendering alone?
No. A rendering confirms design intent but cannot demonstrate real surface texture, fixture fit, local flatness, visible finish or packing contact. Use it to align artwork, then approve a physical production-equivalent sample.
Does a successful first-off apply to every batch?
It applies only while the approved component, surface, artwork, fixture and agreed handling conditions remain controlled. A revised resin, coating, tool, artwork or packing arrangement should trigger a comparison with the retained sample.
What should an importer verify before shipment?
Check the part version, artwork revision, print placement, visible appearance, functional keep-out zones, face protection and carton configuration against the approved reference. Record any agreed sampling method before inspection starts.
Conclusion
UV printing smart home device housings becomes a manageable B2B sourcing project when the buyer and factory work from the actual part, a released artwork file, a retained first-off and a concise inspection plan. That process creates evidence for the project at hand and avoids overpromising based on a generic material label.
Technical resources and next steps
Continue with our UV printable materials guide, supplier qualification checklist, and plastic-part QC checklist.
For independent technical background, review Epson's UV flatbed overview, Roland's smartphone-case handling guidance, and Mimaki's adhesion guidance. Validate every production decision on the actual blank and approved sample.