UV printing white ink coverage inspection / BUYER GUIDE
White-Ink Coverage Inspection for Dark Plastic Parts: Opacity Without Guesswork
White-Ink Coverage Inspection for Dark Plastic Parts. Practical OEM sample, fixture, inspection and export checks for flat plastic parts.
Introduction
UV printing white ink coverage inspection should be qualified on the real production component, rather than from a material label, a digital rendering or a generic coupon. For black or coloured hard-plastic housings needing opaque brand graphics, PaintNex begins with the final blank, a marked printable zone, the released artwork, handling expectations and the buyer's written acceptance criteria. This guide explains how a procurement team can convert those inputs into a defensible sample and an inspectable batch plan.
Direct answer for buyers
The practical question is whether uneven underbase, visible dark substrate through colour, halo around the white layer or inconsistent batches can be assessed on the actual component before production. A dependable answer comes from a product-specific trial: use the intended blank, its final surface, the correct artwork revision, a repeatable orientation and the agreed handling or packing conditions. It does not come from a blanket statement that one material name is always compatible.
The decision that makes this project different
A bright orange graphic may look correct on a white proof but muted on a black enclosure. An underbase can improve opacity, yet poor layer alignment may leave a white fringe at the edge. The buyer should provide the actual dark blank, approved colour reference and white-mask intent. State whether the white should be completely hidden beneath colour or intentionally visible. A transparent acrylic part adds a separate viewing-side question; it should not be approved from the same dark-plastic sample.
Production-equivalent comparison
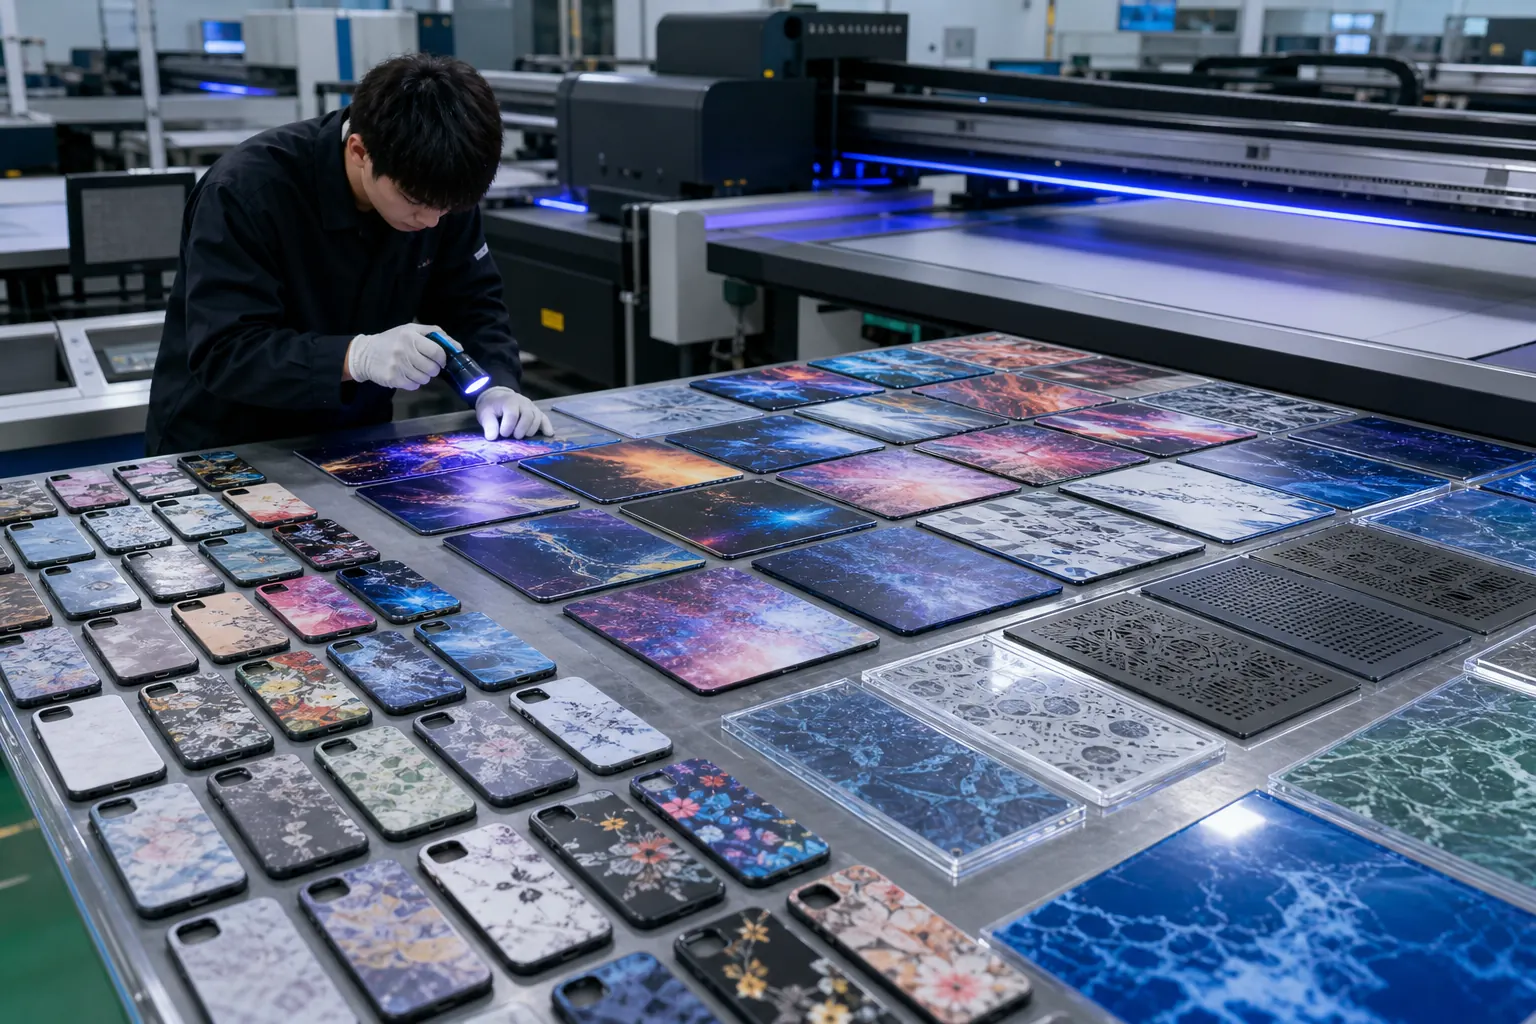
Compare several parts under the agreed lighting and viewing angle. Inspect dense colour fields, small reversed gaps, edges and any gradient transitions where substrate show-through is noticeable. Record the artwork and white-mask revision along with the print order and blank colour. If opacity varies, determine whether the cause is a material shade change, file separation, layer registration or print setup before altering the artwork. The Roland UV primer and layered-print guidance is a process or standards reference, not proof of suitability for an untested PaintNex order.
What the purchase order should settle
Approve a physical colour/opacity range on the intended substrate. Do not promise a universal Pantone match or infer that more white layers always improve appearance; added passes can affect texture and production time.
- Release the white mask separately
- Inspect fringes and show-through
- Retain a dark-blank approval sample
Make the inspection decision reproducible
A quality request should identify a decision and the evidence that supports it. Define the production-equivalent substrate, the accepted first-off, inspection lighting, visible face, defect categories, any measured dimension and the person who can release or reject the lot. AQL-style sampling addresses a lot decision; it does not define whether a white halo, edge bleed or wrong artwork version is acceptable. Those visual rules need product-specific examples and an agreed disposition path.
Separate three moments in the record. Incoming inspection asks whether the blank is suitable to enter the decoration process. First-article review asks whether the current setup is correct. In-process checks ask whether it stays correct after material replenishment, file changes or fixture adjustments. Shipment inspection then looks at representative finished and packed pieces against the same reference. Each moment answers a different question, and none should be described as a blanket guarantee of service life.
When a deviation appears, identify the last known good state, isolate suspect pieces, review the blank lot and artwork revision, and choose whether to rework, retest, accept under written concession or reject. Corrective action should address the observed cause, not automatically blame the printer or ink. A concise record of affected quantity, disposition and preventive check is more useful to an overseas buyer than an unsupported claim that the final batch is 'perfect'.
Separate opacity, colour and registration approvals
The buyer should approve three related but distinct outcomes. First, is the white base opaque enough on the actual dark blank for the intended colour? Second, does the colour layer match the approved direction under the agreed light? Third, is the white mask sufficiently registered that it does not create an unintended fringe? A single comment such as 'make the red brighter' cannot diagnose which layer needs adjustment. Save the white mask and colour artwork as controlled files, and record any layer changes in the first-off approval.
Examine several locations on a representative print: a solid colour field, a thin line, a reversed cut-out and the edge of a small logo. The dark substrate can show through differently across these details. If a transparent plastic product is also in the order, decide whether the art will be viewed through the material and whether the white layer is a backing or a visible graphic. It should be treated as a separate sample, not accepted because the same ink file performed on black ABS.
During factory testing, record the blank lot and surface finish. A new black pigment, matte texture or coating can alter perceived colour and adhesion even with unchanged data. For shipment inspection, compare to the retained approved dark-plastic part, not to a paper proof or monitor. This keeps customer requirements tied to the product application and avoids a promise that one white-ink setting produces identical opacity on every hard-plastic surface.
Why the actual moulded part matters
Plastic parts do not behave as rigid metal coupons. Dimensions, form and local position can move with resin behaviour, shrinkage, tooling, cooling and geometry. ISO 20457:2026 describes a plastics-specific approach to moulded-part tolerances and acceptance conditions. For decoration, this means the fixture and artwork safe area should follow the production part, not an assumed nominal outline.
Inputs to send before feasibility review
| Buyer input | Why it changes the review | Factory output |
|---|---|---|
| Production-equivalent blank | Reveals the true surface, texture and local geometry | Usable print area and fixture reference |
| Released artwork | Controls language, colours, white layers and clear zones | Revision-controlled proof and layer plan |
| Assembly and handling brief | Identifies openings, contact areas and exclusions | Sample test and inspection points |
| Quantity and delivery plan | Shapes tooling, in-process checks and packing | Practical batch and shipment plan |
Factory testing and sample approval
Factory testing should reproduce the variables that matter: the intended blank, final finish, printable orientation, artwork revision, fixture location, white or varnish layers where required, and representative handling. Review placement, edge quality, visible finish, clear zones and packing contact on the physical part. Retain the accepted first-off with a short record of the part version, artwork revision and orientation.
When an adhesion comparison is relevant, agree the exact substrate, surface condition, sample preparation, tape, method and pass/fail rule before testing. ASTM D3359 notes that substrate and surface preparation materially affect coating adhesion, and it identifies limitations of tape methods. Treat the result as a controlled comparison for the specified system, not a universal service-life claim.
Product-specific decisions before artwork release
Separate functional and cosmetic zones
Start by mapping the front face into zones. A cosmetic zone is where a buyer expects a controlled appearance; a functional zone may include a window, sensor, touch area, connector, fastener, latch, light path or assembly datum. The two can overlap visually, so the drawing should make the decision explicit. A printed graphic must never be used as a substitute for an engineering clearance or product-function review.
For black or coloured hard-plastic housings needing opaque brand graphics, the most useful artwork file is accompanied by a simple placement drawing. It identifies the printable zone, a conservative safe area, the part orientation, exclusions and any reference edges used for inspection. That information lets the factory build the fixture and lets an overseas buyer assess the first-off from the same evidence.
Make colour approval traceable
Colour requests are often expressed as a brand reference, a screen image or an informal comment. None of these is enough by itself for batch control. If a specific reference is important, provide the source file, intended substrate, white-base expectation and viewing condition. Keep a signed or otherwise recorded visual approval on the actual component rather than trying to reconstruct it from an email screenshot.
The same discipline applies to matte, gloss, texture and opacity. One component may make a colour look different from another, even where the artwork data is identical. The buyer should decide whether the priority is a visual match, a graphic hierarchy or an agreed production range, then state that priority before the first sample is reviewed.
Plan for change control early
A tool revision, resin supplier change, coating update, changed moulder, different artwork language or altered packaging can all invalidate assumptions in a prior approval. Change control does not have to be bureaucratic: identify the changes that touch the printable face or handling path, compare a new first-off with the retained reference and record the disposition before bulk production resumes.
This is especially important when the buyer expects a family of parts to share one visual identity. Similar housings can have different local geometry, window positions and textures. Approving one size or colour does not automatically approve every member of the family. A short matrix of part number, artwork, finish and approval status is more reliable than a verbal "same as before" instruction.
A practical buyer checklist before purchase order release
- Confirm the component version and quantity match the approved sample request.
- Release the exact artwork file, language variant and source of all required icons or information.
- Mark printable areas, clear zones, contact surfaces and functional exclusions.
- Agree the first-off reference, visible inspection condition and any specifically requested comparison test.
- Confirm fixture orientation, in-process check points, packing protection and shipment-inspection timing.
- Establish how revisions and deviations will be communicated before an order moves to batch production.
This checklist does not transfer product design, legal, regulatory or end-use responsibility to the decoration supplier. It gives procurement a more complete record of the information that a factory needs to execute the requested visual work. The more faithfully the approval part matches the shipped part, the more useful the retained sample becomes when the batch is reviewed.
Mid-article CTA: Request a Product Review
Email info@paintnex.com with photos of the physical blank or an approved drawing, the resin and finished-surface information, marked print area, released artwork, quantity, expected handling and packing requirements. We can prepare a product-specific sampling, fixture and inspection brief. Start with our UV-printable materials buyer guide and artwork and fixtures guide if the project inputs are still being assembled.
From approved sample to repeatable batch
1. Freeze the part and artwork version
Record the component revision, surface finish, artwork file and print orientation. When any one changes, compare the new condition with the retained approved first-off before relying on a previous approval.
2. Validate the fixture on representative blanks
Check more than one blank in the intended fixture. A part can sit differently because of local form, gates, tooling variation or assembly features. A fixture supports repeatable placement; it does not erase the need to identify variation that affects the cosmetic zone.
3. Inspect where the buyer will look
Agree the visible face, inspection lighting, viewing distance and defects that matter. Inspect representative pieces for artwork version, position, edge quality, colour appearance, unwanted marks and excluded functional zones. Use a documented quality-control checklist, not a last-minute visual impression.
4. Include pack-out in shipment inspection
The decorated face can be acceptable at the press and still be damaged by stacking, dividers, bags or carton movement. During shipment inspection, review product protection, carton arrangement and representative finished pieces together. Our export packing guide explains the questions worth closing before release.
Common procurement mistakes
| Shortcut | Why it causes risk | Better control |
|---|---|---|
| Approving a coupon only | It hides real geometry and surface variation | Approve the production-equivalent component |
| Sending artwork without keep-outs | It can place graphics over windows or contact zones | Mark printable and excluded regions |
| Treating a material name as a pass result | Coatings and moulding conditions vary | Test the exact part version |
| Inspecting only before packing | Contact damage can occur after decoration | Run a packing trial and shipment inspection |
FAQ
Why does the same colour file look different on black and white plastic?
The substrate influences the visible result unless the approved ink stack provides sufficient opacity; compare physical samples on each blank.
Can this type of part be approved from a rendering alone?
No. A rendering confirms design intent but cannot demonstrate real surface texture, fixture fit, local flatness, visible finish or packing contact. Use it to align artwork, then approve a physical production-equivalent sample.
Does a successful first-off apply to every batch?
It applies only while the approved component, surface, artwork, fixture and agreed handling conditions remain controlled. A revised resin, coating, tool, artwork or packing arrangement should trigger a comparison with the retained sample.
What should an importer verify before shipment?
Check the part version, artwork revision, print placement, visible appearance, functional keep-out zones, face protection and carton configuration against the approved reference. Record any agreed sampling method before inspection starts.
For an adjacent buyer question, review our related PaintNex guide before releasing the final supplier brief.
Conclusion
UV printing white ink coverage inspection becomes a manageable B2B sourcing project when the buyer and factory work from the actual part, a released artwork file, a retained first-off and a concise inspection plan. That process creates evidence for the project at hand and avoids overpromising based on a generic material label.
Technical resources and next steps
Continue with our UV printable materials guide, supplier qualification checklist, and plastic-part QC checklist.
For independent technical background, review Epson's UV flatbed overview, Roland's smartphone-case handling guidance, and Mimaki's adhesion guidance. Validate every production decision on the actual blank and approved sample.