UV printing supplier checklist / BUYER GUIDE
How to Qualify a UV Printing Supplier: A Practical Checklist from Sample to Shipment
Use this UV printing supplier checklist to evaluate feasibility, samples, fixtures, quality control, packaging, and shipment inspection before placing an order.
Introduction
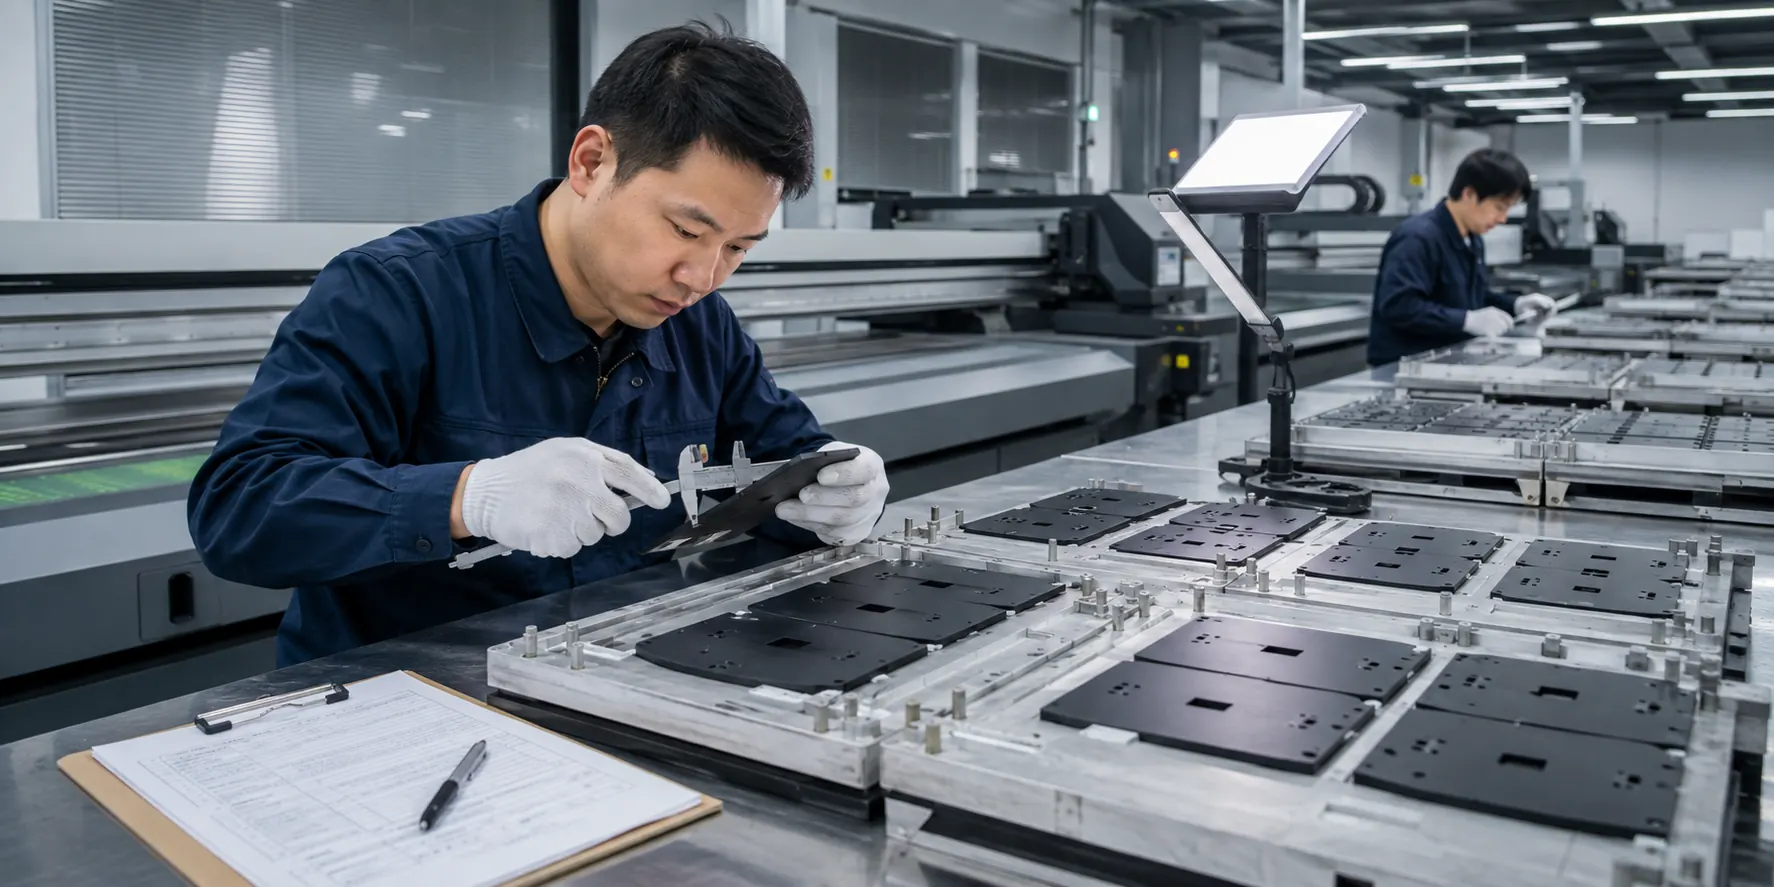
Choosing a UV printing supplier is not simply about finding a factory with a flatbed printer. For custom product decoration, the critical capability is a controlled workflow: understanding the substrate, preparing the item, holding it consistently, managing artwork, inspecting the result, and protecting it through packing and shipment.
This is especially important for cross-border sourcing. A buyer may approve a beautiful first sample and still experience avoidable problems later: artwork placed a few millimeters off, white ink that looks different on a revised coating, rubbing marks caused by packing, or a repeat order that no longer matches the original sample. Those failures are rarely solved by asking a supplier to “be more careful.” They are solved by making the requirement observable before mass production.
This guide provides a practical supplier-qualification checklist for UV direct-to-object printing. It is written for overseas buyers who need custom decoration on products such as promotional goods, consumer accessories, packaging components, panels, cases, gifts, and brand merchandise.
The Short Answer: What Does a Qualified UV Printing Supplier Look Like?
A qualified UV printing supplier can explain the feasibility of your exact product, produce a documented production-equivalent sample, identify the fixture and artwork controls needed for repeatability, agree an inspection standard, and show how printed goods are protected through packing and shipment. The supplier should be willing to state assumptions and limits instead of promising universal adhesion or perfect color without testing.
Qualification is an evidence-gathering process. It starts with your technical brief and ends with a reference sample, production records, and shipment inspection criteria. The aim is not to eliminate every risk; it is to expose the important ones early enough to control them.
Step 1: Send a Brief That Can Be Tested
Many decoration projects begin with a product photo and a logo. That is enough to start a conversation, but it is not enough to quote or qualify a production process reliably. Give suppliers the information that changes feasibility.
Minimum information for a first feasibility review
- Product photos from multiple angles, or a drawing with stable dimensions
- Material, surface finish, color, and any coating information
- A physical sample when the product has complex geometry or an uncertain finish
- Printable area, artwork position, and orientation reference
- Production artwork in the appropriate file format, plus color references if needed
- Quantity by SKU, version, and delivery batch
- Target use: display, promotional giveaway, handled consumer good, component, and so on
- Target market and any known customer, retailer, or compliance requirements
- Packaging concept, especially when printed faces may touch other products
- Desired delivery timing and whether repeat orders are expected
The most important word in this list is finished. A print may behave differently on a production coating than on a bare substrate or early prototype. Where material details are unavailable, say so clearly and make a material check part of the sample plan.
Step 2: Evaluate Feasibility Before You Evaluate Price
Price becomes meaningful only after the supplier understands the product. During a feasibility discussion, listen for specific questions. A capable supplier should ask about the product finish, print zone, curvature, height variation, expected handling, artwork features, and production quantity. Those questions are signs of process thinking, not unnecessary delay.
Questions a supplier should be able to answer
- Can the exact print zone be reached? Ask about print-head clearance, edges, seams, recessed areas, and fixture approach.
- How will the product be held? Request a description or drawing of the jig/fixture concept for repeatable placement.
- What surface preparation is planned? This may include cleaning, treatment, or primer where appropriate. Ask for the step to be recorded, not for proprietary chemistry.
- How will white, clear, or layered artwork be managed? Clarify underbase, registration, and the expected visual result.
- What could cause variation? Good suppliers name realistic limits such as natural-material variation, coating changes, tight curves, or small text near edges.
- What will be checked at first article and before shipment? Look for concrete checkpoints rather than an undefined promise of quality.
If the supplier offers only general statements—“we can print anything,” “it is fully durable,” or “color will be exact”—move the conversation back to the actual product and request a physical sample. A credible supplier is comfortable defining conditions.
Step 3: Build a Production-Equivalent Sample Plan
A sample should answer production questions, not merely create a sales photograph. The best sample plan uses the intended product, artwork, location, finish, and packaging condition as closely as possible.
What to include on the sample
Use final or near-final artwork. Include the real logo, fine text, color fields, gradients where relevant, and any white or clear effect. Print it at the intended location and orientation. If a design will appear close to an edge, seam, button, handle, or curved shoulder, put that challenge in the sample rather than avoiding it.
For products with multiple material lots or natural variation, test a representative set. One flawless natural-wood sample does not predict the appearance of a mixed production lot. One early plastic prototype does not prove the finish of the final molding supplier. Record what was actually tested.
What to document during factory testing
Ask the supplier to record enough information to reproduce the approved condition:
- Product and material identification, including lot or revision where available
- Artwork version and placement reference
- Preparation steps used on the sample
- Fixture or jig reference
- Print and cure process reference (without requiring confidential formulas)
- Photos under agreed lighting before and after test handling
- Test method, condition, and acceptance result agreed by buyer and supplier
- Sample date, reviewer, and retained-sample identification
This record is valuable on a repeat order. It tells the factory what result was approved and gives the buyer a basis for resolving a variation without relying on memory.
Step 4: Turn “Quality” into Checkpoints
Quality requirements become manageable when they are visible. Instead of writing “high quality printing,” break the requirement into features that an inspector can see or measure.
Visual inspection checkpoints
Consider the following points for a product-specific inspection standard:
- Artwork position measured from an agreed physical datum
- Rotation or skew relative to product edges or features
- Print coverage and white-underbase consistency
- Color appearance against the approved reference under agreed lighting
- Fine text, line work, gradients, and image detail
- Banding, pinholes, dust, splatter, curing marks, and unwanted gloss variation
- Edge sharpness and overspray near the print boundary
- Damage caused by loading, unloading, or intermediate handling
Define which defects are critical, major, or minor for your product. Also define the viewing distance. A tiny flaw that is invisible in normal use may not deserve the same disposition as a misplaced logo visible at retail distance. The aim is a fair, repeatable standard—not a vague invitation to dispute every item.
Functional and handling checks
The right check depends on the application. A supplier may propose controlled adhesion checks, rub or handling checks, bend checks for flexible items, packing simulation, or exposure checks relevant to the product. Agree the condition, method, sample quantity, acceptance rule, and reporting format before production.
For coating adhesion, buyers may encounter tape-test references such as ASTM D3359. It is useful as an example of a documented adhesion method, but it should not be copied blindly. Confirm whether the substrate, coating thickness, product geometry, and target market make the selected test appropriate. If the final customer has a required protocol, that protocol takes priority.
Step 5: Review Production Controls, Not Just Equipment Photos
Machine photographs are not proof of repeatable output. During supplier review, ask how the factory prevents predictable variation.
Artwork control
Ask how final files are versioned, approved, and protected from unintended changes. The order record should identify the approved artwork, color target, printable area, and proof date. For variable-data jobs, specify who validates the data file and how failed or duplicate records are handled.
Fixture control
On direct-to-object projects, fixture design often determines placement consistency. Ask whether the fixture is dedicated, how it is identified, whether it uses repeatable locating points, and how the part is checked for seating before print. If a fixture changes, treat that as a controlled change and verify it against the golden sample.
Change control
Products change. A new plastic lot, revised coating, different supplier, new artwork, or modified package can affect output. Ask the supplier to notify you before material or process changes that could alter the approved print result. A short confirmation sample can prevent a much larger repeat-order problem.
Step 6: Prepare for Shipment Inspection and Packing
A product can leave the print station in good condition and arrive with rub marks, blocking, abrasion, dust, or packing pressure damage. This is why packing is part of the decoration qualification, not a separate afterthought.
A practical shipment-inspection routine
Before shipment, compare selected pieces to the approved golden sample. Check artwork version, position, appearance, cure-related defects, and packing protection. Verify that any protective film, tissue, divider, tray, or polybag does not damage the printed surface during normal packing pressure and transit vibration.
For high-value or brand-sensitive orders, agree whether the buyer, third-party inspector, or supplier quality team will perform the final inspection. Define the sampling plan and inspection report in advance. The report should show not only attractive finished goods but also representative packaging and any identified nonconformities with disposition.
What to ask for in a pre-shipment report
- Order quantity and quantity inspected
- Approved artwork and golden-sample reference
- Product and printed-area photos from representative units
- Placement and appearance observations
- Test or handling-check records agreed for the order
- Defect summary and corrective action, if applicable
- Packaging photos, carton marks, count, and shipment-ready condition
This level of reporting is not a substitute for independent inspection when one is needed. It is a foundation for transparent communication and a better handoff between factory, buyer, and logistics partners.
Step 7: Structure the Commercial Agreement Around the Approved Sample
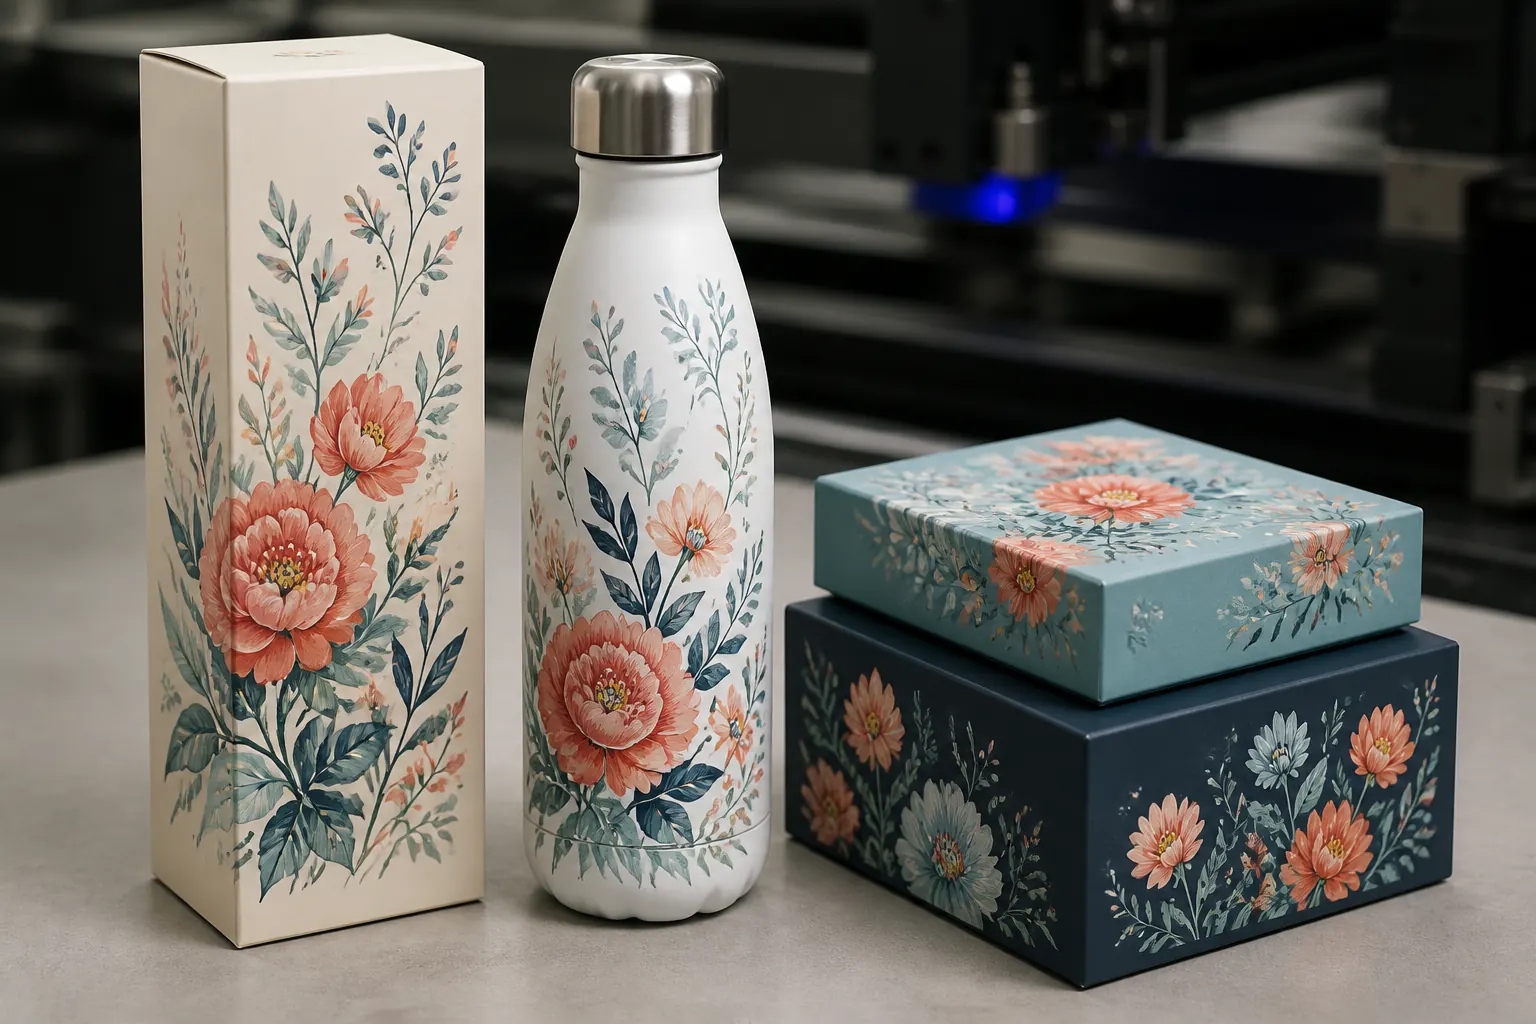
Once technical feasibility is confirmed, make sure the quote and purchase order preserve what was approved. The commercial document should identify the product revision, decoration method, artwork version, print location, quantity by SKU, packaging, lead time, sample approval date, inspection basis, and change-notification expectations.
Avoid relying on photos pasted into chat messages as the only specification. They can be useful references, but they rarely establish scale, version control, or acceptance criteria. A simple controlled specification pack can be more valuable than a lengthy contract if it is accurate, shared, and used on the production floor.
UV Printing Supplier Qualification Checklist
| Qualification area | Evidence to request | Decision signal |
|---|---|---|
| Product feasibility | Review of actual item, finish, print zone, and geometry | Supplier explains limits and fixture approach clearly. |
| Sample quality | Production-equivalent physical sample with final artwork | Appearance is approved on the real product, not only a swatch. |
| Surface preparation | Documented preparation/primer approach where used | Process is traceable for repeat orders. |
| Artwork control | Versioned proof and placement reference | Correct file and location can be verified. |
| Fixture repeatability | Fixture reference and seating/check method | Placement is controlled rather than judged by operator memory. |
| Inspection | First-article and shipment-inspection checkpoints | Defects and acceptance rules are observable. |
| Packaging | Pack-out trial on printed goods | Decoration is protected after it leaves the printer. |
| Change control | Notification and re-approval process | Material or artwork changes do not silently reset quality. |
FAQ
What should I ask a UV printing supplier before placing an order?
Ask whether your exact product and print zone are feasible, how it will be fixtured, what preparation is needed, what sample tests are proposed, how artwork and placement are controlled, and how goods are inspected and packed. Provide the finished product information so the answers are meaningful.
Is a factory sample enough to approve mass production?
It is an important start, but a sample alone does not control a production order. Retain it as a golden sample and pair it with a written specification, fixture/artwork references, inspection points, packaging requirement, and change-control expectation.
How can I check print placement on a shaped product?
Set physical datum points: edges, seams, buttons, openings, or a measured coordinate system. Define allowable variation only after you understand the product’s normal manufacturing tolerance. Visual phrases such as “centered” should be converted into an inspectable reference.
What should a pre-shipment inspection include?
It should compare representative production units with the approved golden sample and check artwork version, placement, visual defects, agreed handling tests, pack-out protection, counts, and carton marks. Agree the sampling method and report format before production.
Should I require a certification from every supplier?
Ask for current evidence relevant to your product and market. A certification can be useful, but it does not replace product-specific sampling and inspection. Do not assume a certification, compliance status, or test result without seeing the current document and confirming its scope.
Conclusion
The strongest UV-printing supplier relationship begins with a clear product brief and ends with a controlled, inspectable production reference. Do not qualify a factory only by equipment photos, price, or a generic durability promise. Qualify the workflow: feasibility, sampling, surface preparation, fixture control, artwork control, inspection, packing, and change management.
Technical resources and next steps
Continue with our UV printable materials guide, supplier qualification checklist, and plastic-part QC checklist.
For independent technical background, review Epson's UV flatbed overview, Roland's smartphone-case handling guidance, and Mimaki's adhesion guidance. Validate every production decision on the actual blank and approved sample.