UV printing vacuum metallized plastic / BUYER GUIDE
UV Printing on Vacuum-Metallized Plastic Panels: Questions Before Sampling
A practical B2B guide to evaluating direct UV decoration on vacuum-metallized plastic panels, including factory testing, sample approval, artwork control, inspection and export preparation.
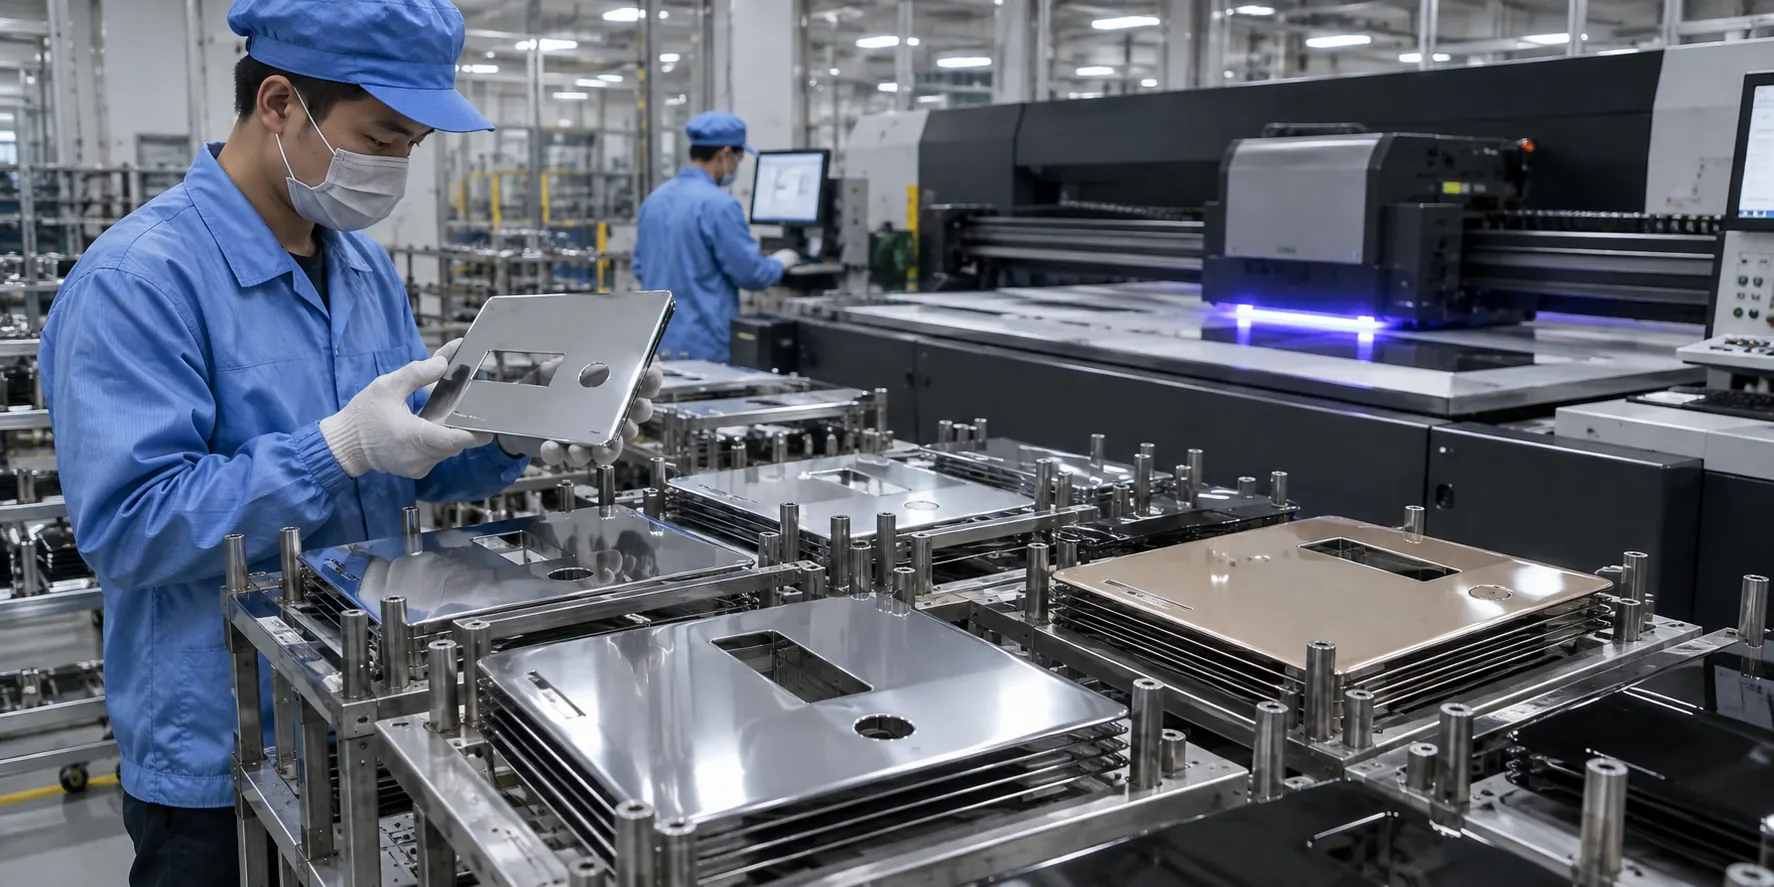
Direct answer for procurement teams
The key decision is whether the final metallized surface, coating system, visible finish and production fixture justify a product-specific sample. The right factory test is a controlled comparison, not a universal compatibility promise. A physical blank makes texture, local flatness, coatings, assembly features and handling conditions visible before a production batch is committed.
What to send for a feasibility review
| Buyer input | Why it matters | What the factory should confirm |
|---|---|---|
| Production-equivalent blank | Reveals the final surface and geometry | Usable print area, head clearance and fixture location |
| Final artwork | Controls language, colour, white and finish layers | Exact revision and keep-out boundaries |
| Handling brief | Defines real contact and cleaning exposure | Sample-review and pack-out conditions |
| Quantity and timing | Shapes fixture and inspection planning | Repeatable batch workflow |
Plastic dimensions, form and location can vary due to material behaviour, moulding shrinkage, processing and geometry. ISO 20457:2026 provides a plastics-specific framework for tolerances and acceptance conditions. For a decoration project, use that reality to define a product-specific fixture and artwork safe area rather than treating all nominally similar parts as identical.
Material, surface and artwork questions
The material name alone is not enough. A change in pigment, mould texture, coating, film, moulder or local feature can alter visible colour, adhesion comparison, registration and fixture support. Provide the actual part version and mark all openings, windows, raised edges, clips, button areas and contact zones before first-off printing.
Colour and finish need a defined viewing condition
If the cosmetic result matters, retain an approved printed part and state how it is compared: for example under neutral light, at an agreed viewing distance and on the intended surface. ASTM D523 describes specular gloss measurement and notes that surface appearance also involves reflection haze and texture. Any instrument, angle or tolerance should be agreed by the responsible quality parties for the final component.
Controlled marks need controlled ownership
When artwork includes instructions, symbols, caution graphics or localized text, the buyer must provide the approved source file and identify the programme owner. A decorative print supplier should not infer a compliance meaning from an icon. For example, the ESD Association's ANSI/ESD S8.1 overview distinguishes awareness symbols with different meanings; the responsible product or ESD programme owner must select the correct content and location.
Factory testing: what a useful sample proves
A useful sample uses the intended part, artwork revision, fixture reference, white or varnish layers where applicable and a practical handling condition. It lets reviewers assess print placement, edge quality, visible finish, protected zones and packing contact. The factory should retain the approved first-off alongside a short record of the part, artwork and orientation used.
Where a tape adhesion comparison is relevant, agree the exact blank, surface preparation, tape, method and visual rule before testing. ASTM D3359 notes that substrate preparation, tape, peel angle, peel rate and operator practice can affect the result; it is a controlled comparison tool rather than a universal in-service durability claim.
Mid-article CTA: Request a Product Review
Send the physical blank or a verified drawing, material and surface information, marked printable area, final artwork, target quantity and packing expectation. PaintNex can turn those customer requirements into a product-specific sample, fixture and inspection brief. See our materials buyer guide and artwork and fixtures guide for related preparation.
A repeatable batch workflow
- Confirm the approved part version, artwork revision and orientation.
- Check several blanks in the selected fixture before release.
- Review the first-off against the retained approval reference.
- Inspect representative pieces for placement, visible finish and keep-out zones.
- Protect the decorated face and confirm carton configuration during shipment inspection.
If the part, surface, artwork, fixture or handling requirement changes, repeat the review as necessary. This is change control: a prior sample is useful only while the product conditions it represents remain controlled.
FAQ
Can this be approved from a rendering alone?
No. A rendering can establish design intent, but it cannot prove the actual surface condition, local geometry, fixture fit, visible finish or packing contact. Use it for artwork alignment and approve the physical production-equivalent sample separately.
Does a passing sample apply to every future batch?
Only when the part version, material or coating, artwork, fixture and handling conditions remain unchanged. A changed blank or process condition should be compared with the retained approved reference before the batch is released.
What should an importer inspect before shipment?
Compare representative finished parts with the approved sample and written criteria. Check part version, artwork revision, position, visible defects, functional exclusions, face protection and carton arrangement. Our pre-shipment inspection guide explains why the product and pack-out should be reviewed together.
Conclusion
evaluating direct UV decoration on vacuum-metallized plastic panels becomes more reliable when the buyer and factory agree on the real component, an artwork safe area, a retained first-off and a simple inspection plan. That provides a clear, evidence-based route from sample approval to repeatable production without overstating what a generic material claim can prove.
Technical resources and next steps
Continue with our UV printable materials guide, supplier qualification checklist, and plastic-part QC checklist.
For independent technical background, review Epson's UV flatbed overview, Roland's smartphone-case handling guidance, and Mimaki's adhesion guidance. Validate every production decision on the actual blank and approved sample.